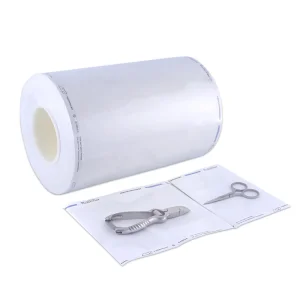
Engineered to deliver ultimate microbial barrier integrity, optimal sterilant penetration, and validated aseptic presentation for healthcare facilities and OEM medical device manufacturers.
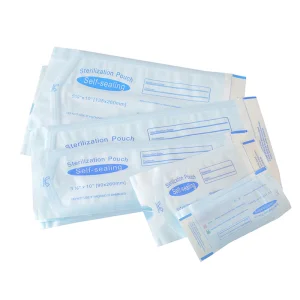

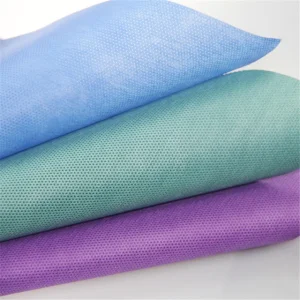
In modern surgical environments and critical healthcare infrastructure, preventing Healthcare-Associated Infections (HAIs) hinges upon one paramount technical standard: maintaining the terminal sterility of medical instruments until the exact moment of point-of-use application. As central sterile supply departments (CSSDs) and medical device original equipment manufacturers (OEMs) adapt to increasingly stringent global regulatory frameworks—such as ISO 11607-1/2, EN 868, and EU MDR 2017/745—the selection of high-performance custom sterile wraps and barrier packaging has evolved from a routine commodity purchase to a high-stakes clinical and risk-management directive.
Clinical Insight: A sterile wrap must maintain a 99.9% Log Reduction Value (LRV) against bacterial penetration, withstand mechanical stress, eliminate linting risks in operating rooms, and facilitate effortless gas/vapor sterilant removal during vacuum phases.
The global sterile wraps market is undergoing unprecedented technological transformation. Traditional single-layer cotton wrappers have been completely phased out in favor of advanced multi-layer nonwoven synthetic polymer matrices (SMS, SMMS, SSMMS) and reinforced medical-grade crepe paper formulations. Modern surgical techniques demand customized packaging solutions that accommodate heavy orthopaedic trays, robotic surgical instrumentation, and intricate endoscopic equipment while maintaining tear resistance and drapeability.
B2B procurement directors, hospital supply chain executives, and quality assurance engineers actively search for custom sterile wrap manufacturers who can bridge the gap between technical compliance and cost efficiency. Key considerations guiding global search intent include:
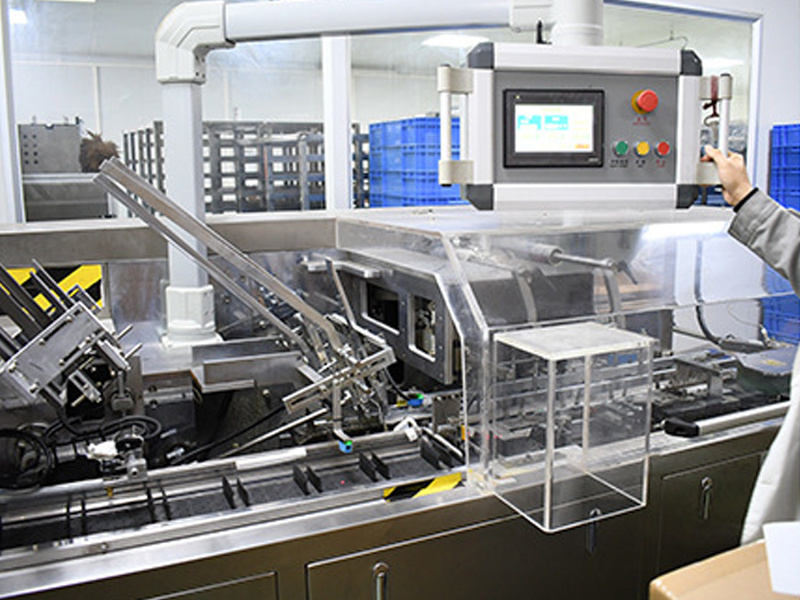
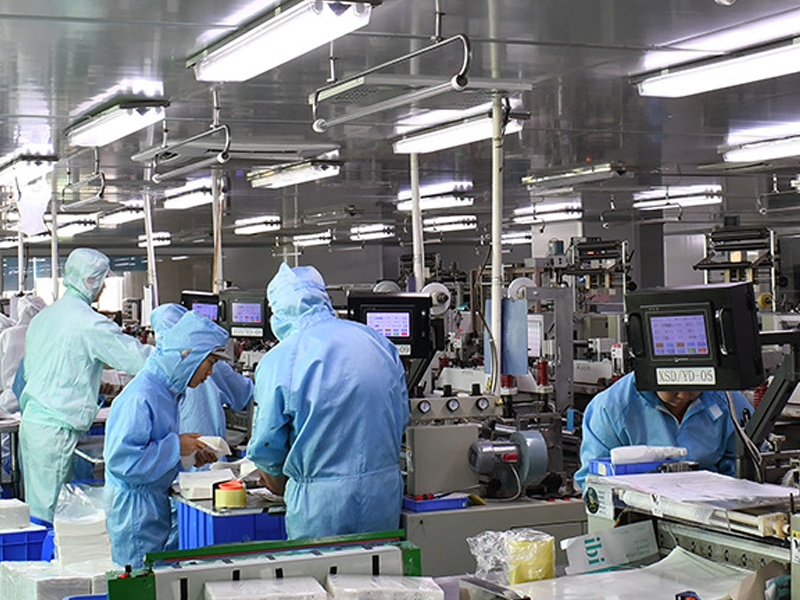
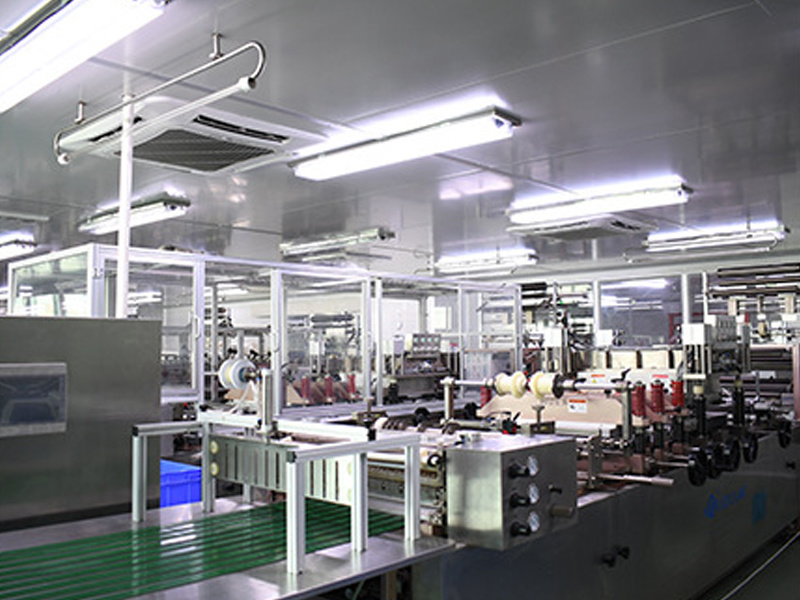
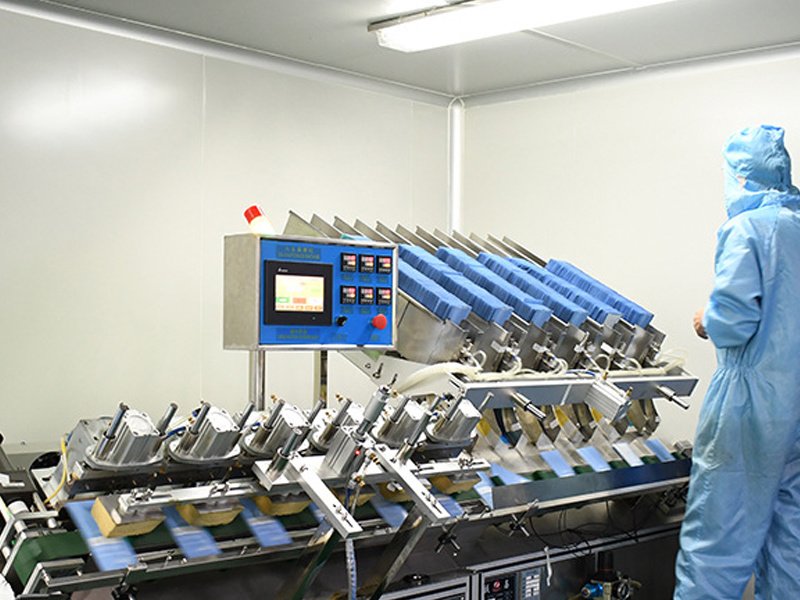
Guangdong Onyx Medical Co., Ltd. is a leading national high-tech enterprise specializing in the research, development, production, and supply of advanced materials for the personal care, medical, and electronics industries. Since its establishment, the company has adhered to a core philosophy of innovation and quality, dedicated to providing high-quality products and solutions to customers worldwide. Located in Guangdong, China, the company operates a modern manufacturing facility covering over 60,000 square meters, equipped with three Class 100,000 cleanrooms and more than 30 PLC-controlled automated production lines. This state-of-the-art infrastructure ensures that every production process meets the highest levels of precision and safety, adhering to international standards.
Proprietary nonwoven SMS and medical-grade paper treatments designed for optimized porosity, tortuous-path microbial filtration, and extreme fluid repellency.
Over 30 PLC-controlled automated lines featuring inline laser inspection systems that eliminate human error, pinhole defects, and weight variations.
Operating within ISO 13485 certified Class 100,000 cleanrooms. Every lot undergoes physical, microbial, and chemical testing prior to dispatch.
Guangdong Onyx Medical is structured into multiple specialized divisions, each committed to addressing the unique needs of its respective industries:
Guangdong Onyx Medical operates under the guiding principles of "Technological Innovation, Quality First," striving to establish a strong brand presence in the global market. The company places a strong emphasis on quality control while ensuring that its production processes are sustainable. With a commitment to environmental protection, resource utilization, and social responsibility, Onyx Medical has gained a reputation as a trusted partner in the healthcare, personal care, and electronics industries. The company’s advanced research and development capabilities, coupled with its efficient production systems, continue to drive it forward as a key player in these sectors. Moving forward, Onyx Medical is dedicated to pushing the boundaries of material science, providing innovative and efficient solutions for its customers worldwide.
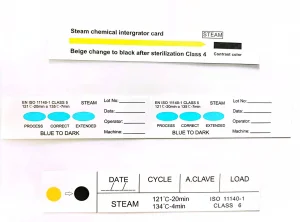
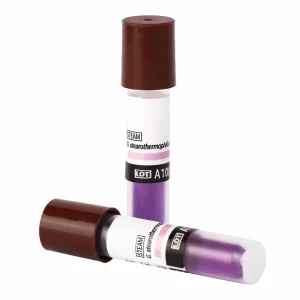
To cater to diverse clinical scenarios—ranging from hospital Central Sterile Supply Departments (CSSD) to outpatient dental surgery center operations—we offer targeted product series integrated with advanced chemical monitoring systems and protective nonwovens.
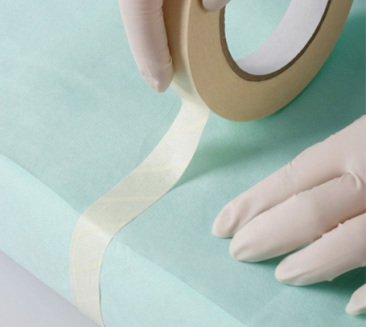
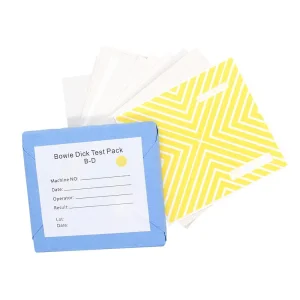
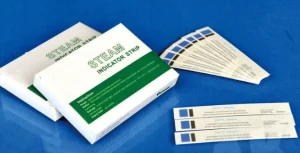
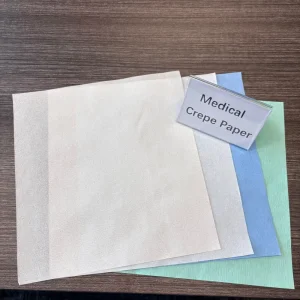
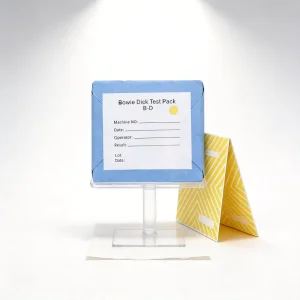
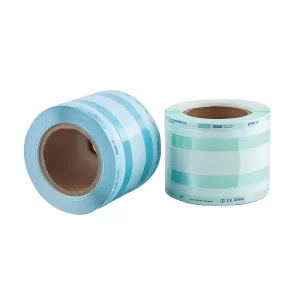
Our vertically integrated manufacturing lines produce high-grade crepe paper, SMS wraps, self-sealing pouch systems, and biological/chemical monitoring packs under strict cleanroom conditions.
Selecting the appropriate custom sterile wrap requires an understanding of material composition, physical properties, and sterilization modality compatibility. Below is an engineering comparison matrix designed for sterile processing managers and OEM buyers:
Constructed via a multi-layer Spunbond-Meltblown-Spunbond matrix. The outer spunbond layers provide high tensile strength and puncture resistance, while the inner meltblown microfiber layer acts as a tortuous path microbial barrier. Ideal for heavy orthopaedic instrument sets, container liners, and harsh handling environments.
Manufactured from 100% virgin cellulose fibers with specialized mechanical creping that imparts elasticity and drapeability. Offers outstanding steam and EO gas penetration with zero memory effect upon opening, allowing smooth aseptic presentation without spring-back contamination risks.
Guangdong Onyx Medical's sterilization wraps and barrier solutions are deployed globally across diverse healthcare environments, meeting localized regulatory standards including US FDA 510(k), CE Mark under EU MDR, and China NMPA certification.
Designed for double-sequential wrapping techniques (AORN recommended) of general surgical sets, micro-instrumentation trays, and basin sets. High tear strength prevents punctures during transit on sterile supply carts.
Custom rolls, pre-cut sheets, and pouches designed for automated cleanroom packaging lines of disposable surgical kits, orthopedic implants, and single-use diagnostic catheters.
Cost-effective self-sealing pouches and lightweight crepe wraps tailored for rapid turnover, steam autoclave cycles, and compact inventory storage.
In-depth answers to critical technical questions asked by medical procurement directors and sterility assurance officers.
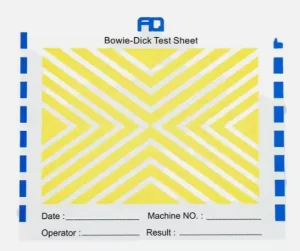
Explore our full line of Bowie-Dick test packs, biological indicators, chemical indicator strips, and low-temperature plasma pouches.

 Onyx Medical